sales@hu-steel.com
 English
 Español
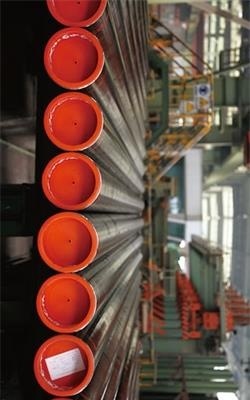
ASTM A53 — Standard Specification for Pipe, Steel, Black and Hot-Dipped, Zinc-Coated, Welded and Seamless.
ASTM A53 covers both welded and seamless carbon steel pipe, available in black or hot-dipped galvanized finishes. It is widely used in mechanical and pressure applications, as well as for ordinary transport of steam, water, gas, and air lines.
The specification categorizes pipes into three manufacturing types: Type F (furnace-butt-welded), Type E (electric-resistance welded/ERW), and Type S (seamless). Available in Grade A and Grade B, Grade A offers better plasticity for cold bending and low-pressure systems, while Grade B provides higher strength and is the preferred choice for medium- and high-pressure industrial applications.
NPS 1/2” – 24” standard (some limitations dependent upon grade).
Sizes up to 26” OD are available on a limited basis.
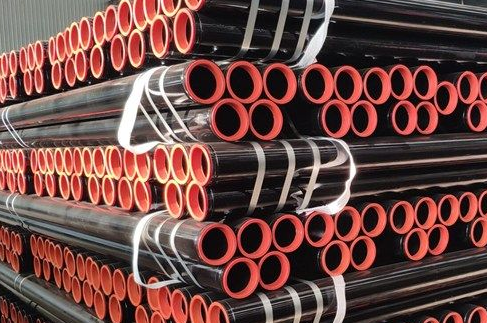
The following types and grades of A53 pipe are covered within this specification:
The chemical composition for seamless (Type S) and ERW (Type E) pipes is strictly controlled to ensure weldability and toughness.
| Type | Grade | C max % | Mn max % | P max % | S max % | Cu max % | Ni max % | Cr max % | Mo max % |
|---|---|---|---|---|---|---|---|---|---|
|
Type S (Seamless) Type E (ERW) |
Grade A | 0.25 | 0.95 | 0.05 | 0.045 | 0.40 | 0.40 | 0.40 | 0.15 |
| Grade B | 0.30 | 1.20 | 0.05 | 0.045 | 0.40 | 0.40 | 0.40 | 0.15 | |
| Type F (Furnace-welded) | Grade A | 0.30 | 1.20 | 0.05 | 0.045 | 0.40 | 0.40 | 0.40 | 0.15 |
(Note: For Type S and E, the sum of Copper, Nickel, and Chromium shall not exceed 1.00%.)
Grade A and Grade B offer different strength levels to suit various pressure requirements.
| Property | Grade A | Grade B |
|---|---|---|
| Tensile Strength, min | 330 MPa (48,000 psi) | 415 MPa (60,000 psi) |
| Yield Strength, min | 205 MPa (30,000 psi) | 240 MPa (35,000 psi) |
| Elongation (min %) | ≥ 35% | ≥ 30% |
Key difference:
Grade B has higher strength (yield strength ≥ 240MPa) and is suitable for higher pressure pipeline systems.
Grade A has better plasticity (elongation ≥ 35%) and is more suitable for cold bending, winding and other forming processes.
ASTM A53 pipes are available in sizes from 1/2" to 26" OD, with standard lengths of 20 ft (6m) or 40 ft (12m). Pipes can be supplied with Plain, Beveled, or Threaded ends.
| Field | Specification |
|---|---|
| Standard | ASTM A53/A53M (ASME SA53) |
| Types & Grades | Type F (Gr. A), Type E (Gr. A, B), Type S (Gr. A, B) |
| Size Range | 1/2" to 24" NPS standard (up to 26" OD available on a limited basis) |
| Wall Thickness | SCH 10, SCH 40, SCH 80, SCH 160, custom |
| Surface Finish | Black (uncoated), Hot-Dipped Galvanized (Zinc-Coated) |
| Length | Single random (4–7m), double random (7–12m), fixed 5.8m / 6m / 12m, custom |
| End Finish | Plain, beveled, threaded |
| NPS (inch) | Outer Diameter (mm) | SCH 40 Wall Thk (mm) | SCH 40 Weight (kg/m) | SCH 80 Wall Thk (mm) | SCH 80 Weight (kg/m) |
|---|---|---|---|---|---|
| 1/2" | 21.3 | 2.77 | 1.27 | 3.73 | 1.62 |
| 1" | 33.4 | 3.38 | 2.50 | 4.55 | 3.24 |
| 2" | 60.3 | 3.91 | 5.44 | 5.54 | 7.48 |
| 3" | 88.9 | 5.49 | 11.29 | 7.62 | 15.27 |
| 4" | 114.3 | 6.02 | 16.07 | 8.56 | 22.32 |
| 6" | 168.3 | 7.11 | 28.26 | 10.97 | 42.56 |
| 8" | 219.1 | 8.18 | 42.55 | 12.70 | 64.64 |
| 12" | 323.9 | 10.31 | 79.62 | 17.48 | 128.07 |
▶ For complete dimensional data, including SCH 10 and SCH 160, refer to our [ERW Pipe Thickness Chart].
ASTM A53 includes hot-dipped galvanized (zinc-coated) requirements for Grade A and Grade B pipes (Grade B is the most common choice for galvanized lines). The zinc coating is applied to both internal and external surfaces through the hot-dip process.
According to Specification ASTM B6, the minimum zinc coating requirements are:
● Total Zinc Coating Weight: Not less than 1.8 oz/ft² (0.55 kg/m²).
● Each Sample Weight: Not less than 1.6 oz/ft² (0.49 kg/m²).
● Individual Surface Weight (Inside/Outside): Not less than 1.3 oz/ft² (0.40 kg/m²).
Choosing the right grade optimizes cost and performance:
ASTM A53 Grade A: Lower strength, better plasticity. Commonly used in construction, low-pressure (≤5MPa) fluid transportation, plumbing pipes, and building structure support.
ASTM A53 Grade B: Higher strength, good pressure resistance. Commonly used in petroleum, chemical industry, machinery manufacturing, medium and high-pressure (≤15MPa) fluid transportation, such as oil and gas pipelines.
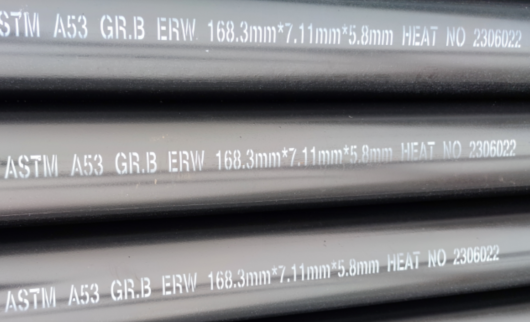
Understanding the differences helps you select the right standard:
| Standard | Service | Temperature | Typical Use |
|---|---|---|---|
| ASTM A53 | General mechanical and pressure applications | Moderate (up to ~400°C) | Water, gas, air, steam lines, structural support |
| ASTM A106 | High-temperature and high-pressure service | High (up to 650°C) | Boiler tubes, high-temperature steam, refinery piping |
| API 5L | Long-distance oil and gas transmission | Ambient to moderate | Petroleum and natural gas pipelines |
Note: ASTM A106 is produced only via the seamless method, whereas A53 includes ERW and seamless. ▶ Learn more about [ERW vs Seamless Pipe: Which One Should You Choose?]
ASTM A53 pipe is versatile and widely used across various industries:
1. Building & Construction: Deep-well pump columns, structural towers, boiler piping, and hot water conveyance lines.
2. Mechanical & Machining: Bearing races, machinery accessories, and general mechanical fabrication.
3. Fluid Transmission: Gas distribution networks, water conduits, and low-to-medium pressure fluid handling.
4. Wind Power: Anti-static piping systems in wind power plants.
The production of ASTM A53 pipe varies by type:
● Seamless (Type S): Manufactured via hot rolling (for thick-wall, large-diameter) or cold drawing (for higher dimensional accuracy and better surface finish).
● ERW (Type E): High-frequency electric resistance welding. The weld is heat-treated (tempered at ≥540℃) to eliminate martensite and ensure toughness. (Suitable for small to medium diameter pipes, such as building pipelines and low-pressure fluid transportation).
● SAW/LSAW: Submerged arc welding (JCOE forming). (Suitable for large-diameter, thick-wall pipes like oil and gas pipelines, offering high weld strength).
▶ To learn more about the ERW welding process, refer to [ERW Steel Pipe Manufacturing Process].
To ensure compliance with ASTM A53, pipes undergo strict testing:
● Hydrostatic Test: Every pipe is tested for pressure bearing capacity to ensure no leakage.
● Non-Destructive Testing (NDT): UT (Ultrasonic), RT (Radiographic), or MT (Magnetic Particle) are used to detect internal or surface defects.
● Mechanical Testing: Tensile, bend, and flattening tests are performed on samples to verify ductility and weld integrity.
ASTM A53 specifies strict mechanical tests to ensure ductility and weld integrity, especially for smaller sizes:
Bend Test: For pipes NPS 2 (DN50) and under, a sufficient length must be capable of being bent cold through 90° around a cylindrical mandrel (diameter = 12 times the pipe OD) without cracking or opening the weld. For close coiling, it must withstand 180° (mandrel = 8 times OD).
Flattening Test: Applicable to pipe over NPS 2 (DN50) up to Extra Strong thickness.
● For Seamless Pipe: Flattened in two steps. No cracks allowed on inside/outside surfaces until the specimen breaks or opposite walls meet.
● For ERW Pipe: Flattened in three steps. The weld is positioned at 0° or 90°. No cracks are allowed at the weld until the distance between plates is less than 2/3 of the specified diameter.
Contact our engineering team for technical support and a fast quotation.
Copyright @2017 Hunan Standard Steel Co.,Ltd and Husteel Industry Group All Rights Reserved