sales@hu-steel.com
 English
 Español
Spiral welded pipe is manufactured by spiral forming a steel strip into a tubular shape and welding the seams with submerged arc welding. The strip is fed at a specific forming angle, allowing pipes of large diameter to be produced from relatively narrow coils. This type of pipe is also commonly referred to as SSAW pipe (Spiral Submerged Arc Welded pipe).
Spiral welded pipes are primarily used for oil and natural gas transmission pipelines. Specifications are expressed as outer diameter × wall thickness. Depending on the application, pipes can be either single-sided or double-sided welded. All finished pipes must meet the required standards for hydrostatic testing, weld tensile strength, and cold bending performance.
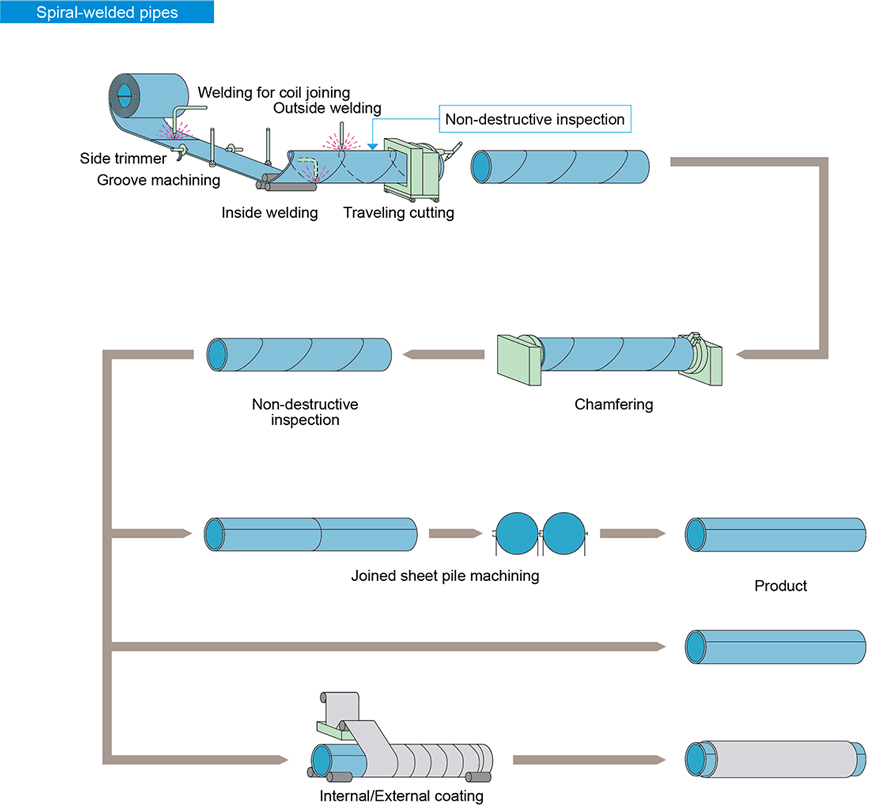
The manufacturing process of spiral welded pipe consists of four main stages:
| Stage | Key Steps |
|---|---|
| 1. Raw Material Preparation | Coil inspection, strip leveling, milling, pre-bending |
| 2. Forming & Welding | Spiral forming, weld gap control, inner & outer SAW welding |
| 3. Inspection & Testing | Online UT, X-ray, hydrostatic pressure test |
| 4. Finishing & Delivery | Plasma cutting, first inspection, pipe end machining |
(1) Raw Material Inspection
The raw materials are strip coil, welding wire and flux. They must undergo strict physical and chemical inspections before being put into use.
(2) Strip Butt Welding
The head and tail of the strip are butted by single-wire or double-wire submerged arc welding, and automatic submerged arc welding is used for repair welding after rolling into a steel pipe.
(3) Leveling, Milling & Pre-Bending
Before forming, the strip is leveled, trimmed, planed, surface cleaned and conveyed and pre-bending.
(4) Strip Conveying Control
The electric contact pressure gauge is used to control the pressure of the cylinder on both sides of the conveyor to ensure the smooth conveying of the strip.
(5) Spiral Forming
Adopt external control or internal control roll forming.

(8) Online Ultrasonic Testing
The welded seams are all inspected by an online continuous ultrasonic automatic flaw tester, which ensures 100% non-destructive testing (NDT) coverage of the spiral welds. If there is a defect, it will automatically alarm and spray the mark, and the production workers can adjust the process parameters at any time accordingly to eliminate the defect in time.
(11) Defect Re-Examination
The parts with continuous sonic flaw detection marks on the welds shall be re-examined by manual ultrasonic wave and X-ray. If they are indeed defective, after repairing, they shall undergo non-destructive inspection again until it is confirmed that the defects have been eliminated.
(12) T-Joint X-ray Inspection
The tube where the strip butt weld and the T-joint intersecting with the spiral weld are all inspected by X-ray television or filming.
(13) Hydrostatic Pressure Test
Each steel pipe undergoes a hydrostatic pressure test, and the pressure is radially sealed. The test pressure and time are strictly controlled by the steel pipe water pressure microcomputer detection device. The test parameters are automatically printed and recorded.
(9) Plasma Cutting
Use an air plasma cutting machine to cut the steel pipe into single pieces.
(10) First Inspection System
After cutting into a single steel pipe, each batch of steel pipes must undergo a strict first inspection system to check the mechanical properties, chemical composition, fusion status of the welds, the surface quality of the steel pipes and non-destructive testing to ensure that the pipe-making process is qualified. Only then can it be officially put into production.
(14) Pipe End Machining
The pipe end is machined so that the verticality of the end face, the bevel angle and the blunt edge are accurately controlled.
a. Uniform deformation, low residual stress
During the forming process, the deformation of the steel plate is uniform, the residual stress is small, and the surface does not produce scratches. The processed spiral steel pipe has greater flexibility in the size and specification range of diameter and wall thickness, especially in the production of high-grade thick-walled pipes and small-to-medium diameter thick-walled pipes.
b. Superior weld quality
Using advanced double-sided submerged arc welding technology, welding can be realized at the best position, and it is not easy to have defects such as misalignment, welding deviation and incomplete penetration, and it is easy to control the welding quality.
c. 100% quality inspection
Carry out 100% quality inspection of steel pipes, so that the whole process of steel pipe production is under effective inspection and monitoring, effectively ensuring product quality.
d. Real-time data monitoring
All the equipment of the entire production line has the function of networking with the computer data acquisition system to realize real-time data transmission, and the technical parameters in the production process are checked by the central control room.
| Item | SSAW (Spiral) | LSAW (Straight) |
|---|---|---|
| Raw Material | Steel strip coil | Steel plate |
| Forming Method | Spiral forming | UOE/JCOE pressing |
| Weld Length | Longer | Shorter |
| Size Flexibility | High | Medium |
| Typical Application | Large diameter, medium wall thickness | High pressure, thick wall |
Hunan Standard Steel Co., Ltd (HSCO) is a leading manufacturer and supplier of carbon steel pipes (seamless and welded), supplying many types, grades, diameters and lengths of pipe to a variety of industries.
● 12 modern SSAW production lines with annual capacity of 400,000-500,000 tons
● Outer diameter: 219mm-3620mm | Wall thickness: 5.0mm-25.4mm | Steel grade: L245-X80
● API 5L, ISO 9001, CE certified
● 100% UT + X-ray + hydrostatic testing on every pipe
Related Resources:
● 3PE Coating Anti-corrosion Steel Pipe Material
Related information
Copyright @2017 Hunan Standard Steel Co.,Ltd and Husteel Industry Group All Rights Reserved