sales@hu-steel.com
 English
 Español
How is a flat steel strip processed into high-quality ERW pipe? Every step is completed on a purpose-built, automated production line, including continuous roll forming, high-frequency welding and final inspection. This setup handles the entire ERW tube manufacturing process. The line produces round, square and profiled carbon steel pipes, including standard ERW line pipe, for construction, petrochemical and light industrial projects.
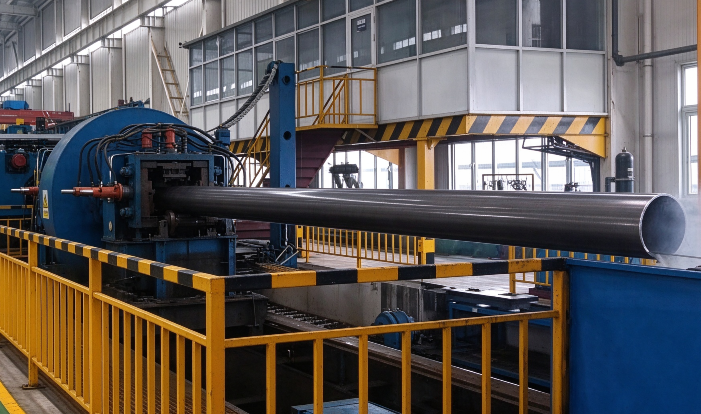
The diagram below illustrates how a steel coil is converted into finished pipe.
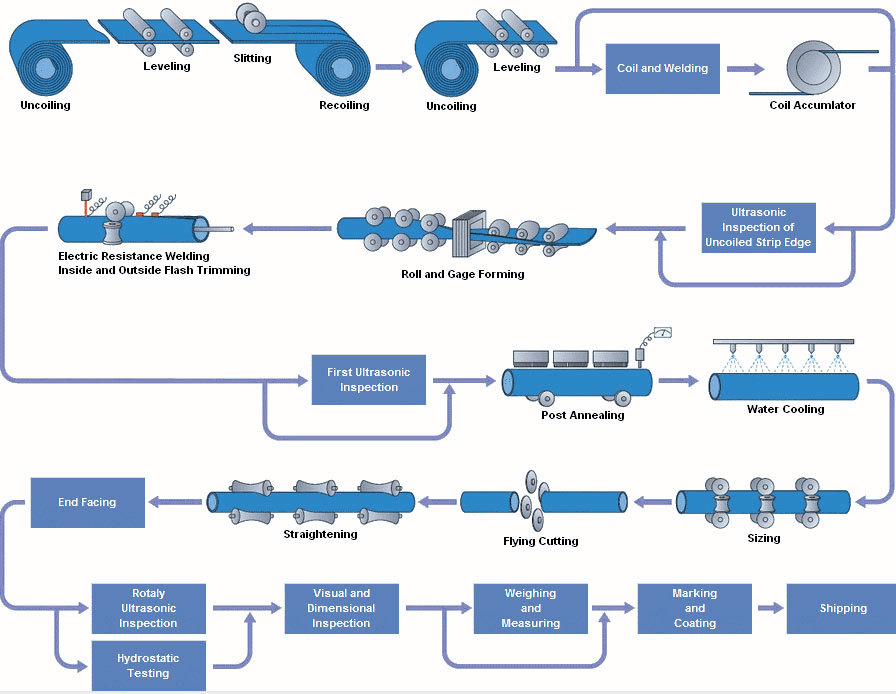
Don't let the long line of equipment intimidate you—it happens in 5 continuous stages:
A complete ERW line is made up of the following machinery:
● Preparation: Decoiler, Strip Leveler, Shear & Butt Welder, and Accumulator (Storage Looper).
● Forming & Welding: Roll Forming Machine, High-Frequency Welder, and Flash Trimmer (for weld flash removal).
● Treatment & Sizing: Post-Weld Induction Tempering System, Water Cooling, and Sizing Machine.
● Cutting & Finishing: Flying Cut-off Saw, Straightening Machine, and Pipe End Facing Machine.
● Testing & Inspection: Online UT Flaw Detection, and Hydrostatic Tester.
Before the steel is formed, it must be prepped.
● Uncoiling & Leveling: The raw steel coil is loaded onto the decoiler. The flat strip passes through leveling rolls to remove any coil curvature.
● Shearing & Butt Welding: To keep the line running non-stop, the tail end of the current coil is sheared straight and welded to the lead end of the next coil.
● Accumulator (Looper): The looper cage stores a loop of steel strip. This allows the mill to maintain continuous line speed while a new coil is being welded.
● Edge Milling & Strip UT: The strip edges are milled clean before welding. An online Ultrasonic Test (UT) scans the strip edge to catch laminations. If a defect is detected, an automatic paint-spraying device marks it, ensuring 100% tracking and removal of defective steel before it enters the mill.
● Roll Forming: The flat strip runs through a sequence of driven roll stands (commonly known as U-forming and O-forming stands), gradually being formed into a cylindrical tube shell.
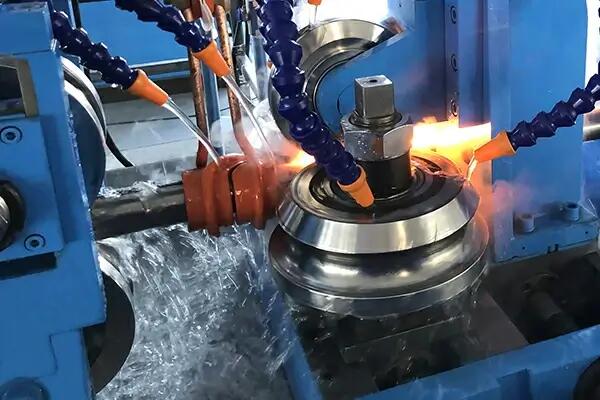
● High-Frequency ERW (Electric Resistance Welding): The strip edges are heated to forging temperature by high-frequency alternating current (typically 100–400 kHz). The skin effect and proximity effect concentrate the current precisely along the strip edges. Squeeze rollers press the heated edges together to form a forged weld joint. No filler metal is required for this process.
● Flash Trimming: Cutting tools remove internal and external weld flash for a smooth weld surface.
The heat of the welding process alters the steel's structure, so it must be treated.
● Post-Weld Induction Tempering: The weld seam is locally heated by an induction coil (usually ≥540°C). This relieves welding stresses, eliminates untempered martensite, and restores weld ductility to a level comparable with the base metal.
● Water Cooling: The pipe passes through water spray rings to cool down rapidly.
● First Online UT: An inline NDT unit scans the just-welded seam and heat-affected zone for flaws. A dedicated laser sensor monitors the internal flash height in real-time for strict process control. (To see how this works, see [NDT Guide for ERW Pipe Welds]).
● Sizing: The pipe passes through sizing rolls to achieve the precise final outer diameter and roundness.
● Flying Cut‑off: A computer‑controlled flying cut‑off saw matches the line speed of the pipe, cutting to standard lengths such as 6 m or 12 m.
● Straightening: The cut pipes are passed through a straightener to eliminate bending.Pipes are straightened either inline before cutting or offline after cutting to eliminate bow and bend.
● End Facing: Pipe ends are milled flat or machined with welding bevels.
● Off-line NDT & Hydrostatic Testing: Pipe ends and bevel surfaces undergo Magnetic Particle Testing (MT) and manual UT to detect cracks in the UT-blind end zones. Every pipe is then hydrostatically tested for leak-tightness. For ASTM A53 pipe, test pressures may reach up to 2500 psi depending on dimensions. (Learn more about the [Limits of Hydrostatic Testing]).
● Visual Check & Coating: Inspectors verify surface and dimensions before applying anti-rust oil or protective coatings. The pipes are bundled and shipped.
Our production line is highly flexible. Here are the standard specifications we can manufacture:
| Parameter | Standard Range | Custom Capabilities |
|---|---|---|
| Outer Diameter (OD) | 21.3mm – 610mm (1/2" – 24") | Up to 660mm on request |
| Wall Thickness (WT) | 1.0mm – 20.0mm | Thicker walls available |
| Standard Lengths | 6m (20ft), 12m (40ft) | Custom cut lengths |
| Steel Grades | ASTM A53 Gr.A/B, API 5L (X42-X70), EN 10219 | Other grades upon request |
| Surface Finish | Black, Hot-dipped Galvanized, 3PE/FBE coated | Bare pipe |
(👉 Need precise wall thickness and weight data? Check out our [ERW Pipe Thickness Chart].)
Don't underestimate the steel coil. To keep the line running non-stop and avoid weld defects, the raw material has to be good. You need clean carbon steel (like ASTM A53 Gr.B or API 5L) with consistent chemistry—meaning tight control over carbon and manganese. If the coil's dimensional precision is off, or if it has severe edge defects, the whole forming and welding process will suffer.
Compared to seamless pipes, ERW pipes are lighter and have tighter dimensional tolerances. If you are evaluating the ERW steel pipes manufacturing plant cost, ERW lines offer excellent cost advantages for high-volume production. This makes them widely used across many sectors:
Because of this, you'll find them everywhere:
● Fluid Transport: Low-to-medium pressure lines (oil, gas, steam, water, air).
● Construction: Scaffolding and structural columns.
● Mechanical: Automotive parts and furniture tubing.
Not sure whether ERW or seamless is right for your project? Learn more in our [ERW vs. Seamless Pipe Guide].
Q1. What is the typical lead time?
A: For standard sizes in stock, it's 7-15 days. For custom sizes or large bulk orders, it's typically 20-30 days depending on the quantity.
Q2. Do you provide third-party inspection?
A: Yes. We fully support third-party inspections (like SGS, BV, Intertek) during production and before shipment. All pipes come with a Mill Test Certificate (MTC) and hydrostatic test reports.
Q3. Can you cut pipes to custom lengths?
A: Absolutely. Our computer flying saw allows us to cut pipes precisely to your required lengths (e.g., 5.8m or 11.8m) without extra delay.
Q4. Why choose ERW over seamless pipe?
A: As mentioned earlier, ERW pipe offers better dimensional tolerance, a smoother surface, and is much more cost-effective, especially for low-to-medium pressure applications.
Whether you are sourcing ERW pipes for a construction project or looking for factory equipment, our engineering team is here to help.
Send us your specifications today and get a fast, competitive quotation within 24 hours.
👉 [Get a Free Quote & Technical Consultation]
Related topics
● ERW vs. LSAW vs. SSAW: Which Welded Pipe is Better? – Compare the manufacturing processes, sizes, and applications of all three types.
● ERW Pipe Thickness & Weight Chart – Check standard dimensions, wall thickness (SCH 40/80), and theoretical weights.
● ASTM A53 GR.B ERW Pipe: Specifications & Applications – Explore the chemical composition, mechanical properties, and uses of this standard grade.
● API 5L ERW Line Pipe Grades – Choose the right grade (X42 to X70) for your oil and gas project.
● BS 1387 Hot-Dip Galvanized Steel Pipe – Learn about the galvanizing process, Class B/C coating, and specifications.
Related information
Copyright @2017 Hunan Standard Steel Co.,Ltd and Husteel Industry Group All Rights Reserved